Manufacturing maintenance software that moves your plant from breakdowns to planned work

Put every press, conveyor, CNC machine, compressor and boiler on a maintenance plan, let operators report breakdowns from the machine, and see backlog, schedule compliance and cost per asset without building a spreadsheet.

Book a demo
Updated 15 Oct 2026
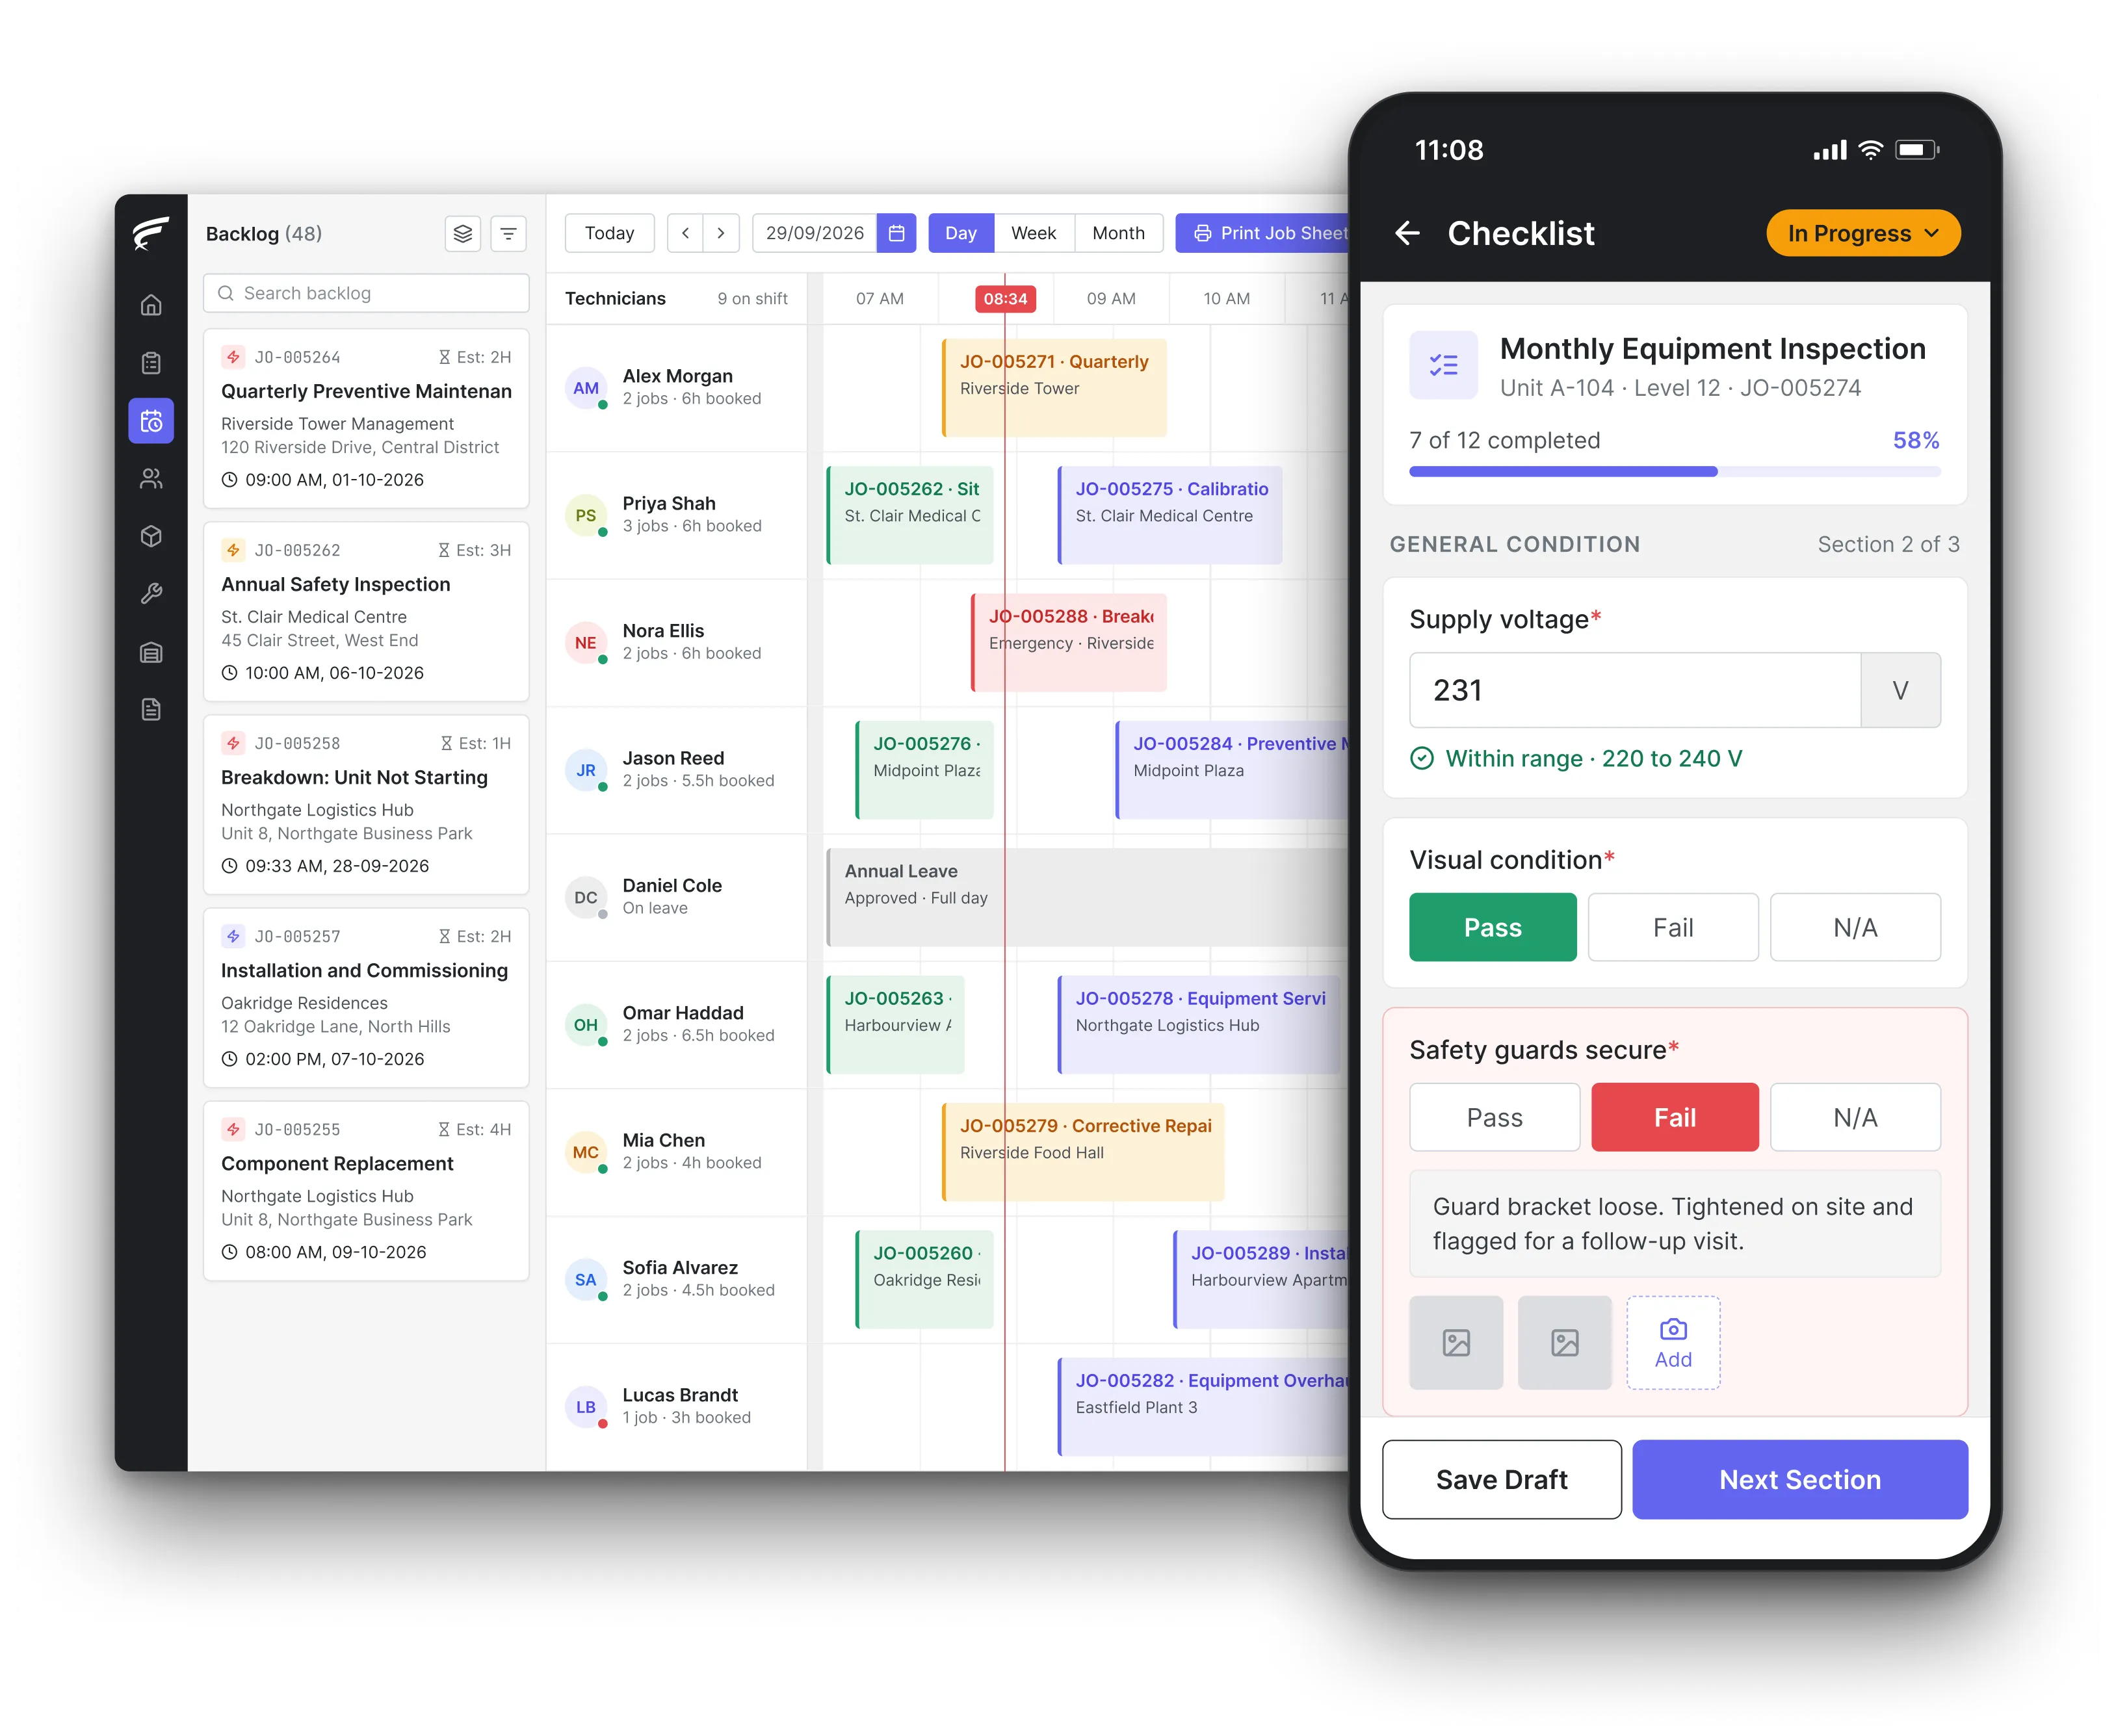
FieldEx scheduling board on desktop with a technician's inspection checklist open on the mobile app, as used by plant maintenance teams

FieldEx is manufacturing maintenance software that brings a computerised maintenance management system (CMMS) and field service management together for factory and plant maintenance teams. It schedules preventive maintenance by run hours, cycles or date, turns operator breakdown reports into assigned work, runs press, crane and pressure-plant inspections, tracks spares in the maintenance store, and reports backlog, reliability and cost for every machine.

What FieldEx does for factory maintenance teams

A factory maintenance team is judged on two things: how little unplanned downtime the lines have, and whether the statutory checks on presses, cranes and boilers were done on time. FieldEx runs both on the same machine records, so the planned service, the breakdown and the inspection that found the worn clutch all sit in one history. Book a demo to see it on your own lines.

Production lines, machines and utilities on record

  • An asset record for every press, injection moulder, CNC machine, conveyor, robot cell, compressor, boiler, chiller and overhead crane, with serial number, specifications, photos, warranty and attached manuals.
  • Line, machine and component levels, so a gearbox, a motor or a clutch keeps its own repair history under the machine, in asset management.
  • Machines grouped by plant, building or line, classified by type and category, with statuses such as running, under maintenance or out of service.
  • QR or barcode labels on each machine, and a change history of who edited what and when.

Planned maintenance by run hours, cycles or date

  • Maintenance plans that trigger on running hours, cycle counts or the calendar, or whichever threshold comes first, in preventive maintenance.
  • Different checklists and technicians for daily, weekly, monthly and annual tasks on the same machine.
  • Fixed calendar schedules for shutdown windows, or schedules counted from the last completed service. Fixed calendar dates apply to time-based plans.
  • Missed maintenance rescheduled after a set overdue period, and each plan showing every machine's last and next service.

Breakdowns reported from the shop floor

  • A QR label on each machine that opens a breakdown request without logging in, with a description, contact details and photos or video.
  • Every request arriving as a job in the backlog, assigned by skill, shift, leave and availability to the right maintenance technician.
  • An alert when a new job repeats a recent job on the same machine, so repeat failures are seen early.
  • Response and repair targets measured in the plant's working hours, with at-risk and violation alerts.

Statutory checks on presses, cranes and pressure plant

  • Recurring inspections and certifications per machine type on standard or custom frequencies, with the examining body recorded.
  • Due, overdue and completed status, with reminders by email, in-app notification or both.
  • The date, the person, the result and remarks on each record, with the thorough examination report attached.
  • Checklists that raise the repair from a failed answer, update the machine's status and meter reading, and book a follow-up inspection.

Maintenance technicians on the shop floor

  • Each job on the FieldEx mobile app with the machine's history, its checklist, number fields for readings such as temperatures, pressures and amps, and watermarked photos.
  • Ordered procedures, with isolation steps that must be completed before the next task starts and designated tasks required before the job can close.
  • Check-in and check-out on each task, so time spent on each machine is recorded.
  • Jobs and tasks can be downloaded and worked offline, with check-in, check-out and travel synced later.

Spares in the maintenance store

  • Spare parts in each store, zone and technician's own stock, with transfers, barcode scanning and approvals where needed.
  • Reorder and low-stock alerts per stock location, and part availability by store or technician, in spare parts inventory.
  • Parts used recorded on each job and machine, with unit prices, manufacturer details and warranty periods.

Downtime, backlog and cost reports

  • Reports on asset reliability, maintenance cost, utilization, age and lifecycle, in reporting and analytics.
  • Job reports grouped by job type, machine, line or period, with counts, sums and averages, to compare planned work against breakdowns.
  • A dashboard of overdue work, work due in the next 7 days and work completed in the last 7 days, filtered by machine type or group.
  • Reports exported as CSV, Excel or PDF, or emailed to plant management on a schedule.

How should a plant track equipment downtime, and what targets are realistic?

Track it as a ratio, not just a number of hours. Pacific Northwest National Laboratory's (PNNL) guide to applying key performance indicators, written for the US Department of Energy's Federal Energy Management Program (December 2020), sets availability, meaning equipment uptime over expected operating time including planned downtime, at a target above 90% and trending upward. Its downtime indicator compares unplanned equipment failures and shutdowns with planned ones, with a target below 25% and trending downward, and planned downtime below 10% of uptime. PNNL's guide to reliability-centred maintenance (May 2022) adds that all time and costs related to operation, downtime, equipment purchases, training, contracting and spare parts inventory need to be tracked.

The ratio only works if every stoppage is logged against the machine, whether it was planned or not.

What FieldEx does about it

  • Planned and unplanned kept apart: planned maintenance jobs come from plans, breakdowns from requests, and each job shows which plan generated it, so the two can be counted separately.
  • Machine status on record: checklists and technicians can set a machine to out of service and back, and the dashboard shows the status breakdown across the plant. FieldEx reports downtime, MTBF and MTTR for every machine.
  • Time on every job: check-in and check-out on each task record how long the machine was being worked on.
  • Costs in one place: parts with prices and labour time are recorded on each job, and maintenance cost reports roll them up per machine or line.

What share of plant maintenance should be planned rather than reactive?

PNNL's discussion of maintenance approaches (July 2021) puts typical industry programmes at 40-60% reactive, 30-50% preventive and 10-15% predictive, and the best programmes at under 10% reactive. Its reliability-centred maintenance guide (May 2022) describes top-performing programmes as under 10% reactive, 25-35% preventive and 45-55% predictive. The earlier US DOE FEMP Operations and Maintenance Best Practices guide (PNNL-13890, December 2002) found that the average programme was more than 55% reactive, 31% preventive and 12% predictive.

Heating surface (single or combined)Person in charge
100 m² or lessSteam boiler operator grade 2
Over 100 to 200 m²Steam boiler operator grade 1, on each shift
Over 200 to 500 m²Operator grade 1, plus engineer grade 1 or 2 (can be visiting)
Over 500 to 2,000 m²Steam boiler engineer grade 1 or 2
Over 2,000 m²Steam boiler engineer grade 1

Most plants don't know their own split, because breakdown work is not logged the same way as planned work.

What FieldEx does about it

  • Every job typed: job types such as preventive, predictive, corrective and breakdown get their own forms and fields, so each job counts in the right group.
  • The split as a report: job reports grouped by type and period show the share of planned against reactive work, month by month.
  • Inspection findings as their own work: corrective jobs raised from a failed checklist answer are linked to the inspection that found the problem.
  • Condition readings logged: temperatures, vibration values and other readings are entered as numbers and kept on the machine's meter history.

How much can preventive and predictive maintenance save over run-to-failure?

PNNL's reliability-centred maintenance guide (May 2022) estimates that a preventive maintenance programme saves 12 to 18 percent over a reactive one, and predictive maintenance a further 8 to 12 percent over preventive. Its maintenance approaches discussion (July 2021), citing FEMP (2010), says a facility relying mainly on reactive maintenance could easily see savings exceeding 30% to 40%. The US DOE FEMP O&M guide (PNNL-13890, December 2002) cites survey results for predictive maintenance programmes of a 35% to 45% reduction in downtime and 70% to 75% of breakdowns eliminated.

PNNL is also clear that accurate records of programme data are the basis for working out those benefits in a given plant.

What FieldEx does about it

  • A baseline from day one: every breakdown, repair and part is recorded against the machine from the first week, so there is a before figure to measure against.
  • Cost per machine: maintenance cost reports per machine, line or asset type show where reactive spending is concentrated.
  • Plans where they matter most: machines with the most breakdowns can be put on preventive plans first, by hours, cycles or date.
  • Results over time: scheduled reports compare breakdowns and costs month on month, emailed to plant management.

How often does a power press need to be inspected, and what records are kept?

In the US, OSHA 29 CFR 1910.217 requires each mechanical power press to be inspected and tested at least once a week to check the condition of the clutch and brake mechanism, the antirepeat feature and the single-stroke mechanism. The employer keeps a certification record of each inspection and each maintenance and repair task, with the date, the signature of the person who did the work and the serial number or other identifier of the press. In the UK, HSE's HSG236 on power press maintenance and thorough examination (second edition, 2003) requires a thorough examination of the press and its guards at least every 6 months, or every 12 months where the tools are fenced only by fixed fencing, and an inspection and test by an appointed person every day the press is in use, within the first 4 hours of each working period.

HSG236 breaks press maintenance into daily, weekly, monthly and six-monthly checks, with some tasks, such as removing the flywheel, at intervals of 2 years or more.

What FieldEx does about it

  • Daily, weekly and six-monthly on one press: the appointed person's daily check, the weekly clutch and brake test and the six-monthly thorough examination run as their own recurring inspections or certifications.
  • The OSHA record fields: each inspection holds the date, the person who did it and the press's identifier, and the technician signs the job on the phone.
  • Long-interval tasks planned: two-yearly tasks such as flywheel removal sit in the same plan as the monthly service, with their own checklist.
  • Faults stop the press on record: a failed clutch or brake answer raises the repair and sets the press's status to out of service.

How often should overhead cranes and hoists in a factory be inspected?

OSHA 29 CFR 1910.179 on overhead and gantry cranes splits inspections into frequent inspections, daily to monthly, and periodic inspections at 1- to 12-month intervals. Hooks and hoist chains get a visual inspection daily and a monthly inspection with a certification record that includes the date, the signature of the person who did it and an identifier. In the UK, regulation 9 of LOLER, the Lifting Operations and Lifting Equipment Regulations 1998, requires lifting equipment to be thoroughly examined at least every 12 months, or every 6 months for lifting accessories and equipment used to lift people.

A shop floor with a dozen hoists and a box of slings has hundreds of small inspections a year, and each needs its record.

What FieldEx does about it

  • Every hoist and sling on record: each crane, hoist, chain block, sling and spreader beam is its own asset with a QR label.
  • Daily, monthly and yearly cycles: visual checks, monthly hook and chain inspections and the 12-month or 6-month thorough examination each run as recurring inspections or certifications.
  • Signed monthly records: the monthly inspection records the date and the person, and the job is signed on the phone.
  • Accessories out of use: a sling that fails its check can be set to out of service, so its record shows it must not be used.

How often should industrial steam boilers and air receivers be tested and examined?

HSE's guide to the safe management of industrial steam and hot water boilers, INDG436 (first published October 2011), says the manufacturer's routine tests should be carried out as a minimum, and more often where water quality is poor. The written scheme for a steam boiler should include an out-of-service examination, cold, off-line and open for inspection, followed by an in-service examination at operating pressure. Test results should be recorded with the operator, the date and any corrective action. HSE's guidance on the Pressure Systems Safety Regulations 2000 says they cover steam at any pressure and compressed gas, including air, above 0.5 bar, and that before using qualifying pressure equipment a written scheme must be in place and an examination done. HSE's INDG261 (rev2, 2012) adds that the examination is not a substitute for regular and routine maintenance.

So a factory's boiler and compressor house carries daily or weekly tests, a two-stage examination and routine servicing on top.

What FieldEx does about it

  • Routine tests logged by the operator: daily and weekly boiler tests run as recurring inspections, with readings as numbers, the operator and the date recorded, and failures raising a corrective job.
  • Two-stage examinations: the out-of-service and in-service examinations are separate tasks on the examination job, in order.
  • Receivers on their own scheme: each air receiver is an asset with its written scheme attached and its examination as a recurring certification.
  • Servicing kept separate: compressor and boiler servicing runs on running hours or calendar dates in its own maintenance plan.

How do you decide how often to inspect production machines?

By risk, use and the manufacturer's advice. HSE's equipment and machinery FAQs on PUWER (updated 7 May 2026) say inspection frequencies depend on the type of work equipment, its use and the conditions it is exposed to, and should be set by risk assessment and the manufacturer's recommendations. HSE describes typical tiers: quick checks before use, weekly checks such as guarding and the function of safety devices, and more extensive examinations every few months or longer. HSG236 adds that the parts of a press and its control system that are essential to safety at the tools need more frequent maintenance than other parts.

The practical result is a different schedule for the safety-critical parts of a machine than for the rest of it.

What FieldEx does about it

  • Tiers on one machine: pre-use, weekly and periodic checks on the same machine each have their own checklist and frequency.
  • Safety-critical components on tighter cycles: guards, interlocks and light curtains can be components with their own, more frequent inspection.
  • Checklists from your procedure: inspection questions can be generated with AI from a PDF or PNG of your existing checklist or procedure, then edited.
  • Frequencies that follow the conditions: a machine in a hot, dusty or high-duty area can be put on a shorter interval than the same model elsewhere.

Do you have to keep a maintenance log for factory machinery?

Not always, but you should for high-risk equipment. HSE's PUWER FAQs say there is no legal requirement to keep a maintenance log, but it is recommended that employers keep maintenance records for high-risk equipment, and where a maintenance log exists the law requires it to be kept up to date. Inspection records under PUWER are kept until the next inspection, according to HSE's brief guide INDG291 (rev1, 2013). For mechanical power presses in the US, OSHA 29 CFR 1910.217 requires certification records of each inspection, maintenance and repair, with the date and the signature of the person who performed the work.

A log that is out of date is worse than none, because it is a legal record that shows work not being done.

What FieldEx does about it

  • A log that keeps itself: every planned job, breakdown, inspection and part used is recorded on the machine as the work is done.
  • High-risk machines flagged: machines can be classified by category, so high-risk equipment can be reported on its own.
  • Signed entries: each job carries the technician's check-in and check-out times and a signature captured on the phone.
  • The log on demand: a machine's maintenance history can be exported as CSV, Excel or PDF.

What lockout steps are required before maintenance on production machines?

OSHA's lockout/tagout standard, 29 CFR 1910.147, requires energy control procedures to be developed, documented and used whenever employees service or maintain machines where unexpected start-up or release of energy could cause injury. The employer must inspect each energy control procedure at least annually and certify that the inspection was done. HSE's PUWER FAQs add that maintenance work should only be done by people who are competent to do it.

On a production line, the lockout is usually the step most likely to be skipped when the line is under pressure to restart.

What FieldEx does about it

  • Isolation before the work: a job can be built as an ordered procedure, with isolation and a try-start test as tasks that must be completed before the maintenance task starts.
  • No closing without the steps: designated tasks, such as removing locks and handing the machine back, must be completed before the job can close.
  • Competent people only: assignment rules send each job to technicians with the matching skill, such as electrical or hydraulic.
  • The annual procedure inspection: each machine's energy control procedure gets a yearly recurring inspection, with the inspector and the date recorded.

Is NFPA 70B electrical equipment maintenance now mandatory?

It is now a standard rather than a recommended practice. The National Fire Protection Association (NFPA) says the 2023 edition of NFPA 70B, Standard for Electrical Equipment Maintenance, became effective on 16 January 2023, and that the move from recommended practice to standard provides more enforceability for what must be done in electrical equipment maintenance. NFPA also notes that NFPA 70E requires a documented electrical safety programme that considers the condition of maintenance of electrical equipment and systems.

For a plant, that puts switchgear, motor control centres and distribution boards on a maintenance plan with records, not just on an emergency call-out list.

What FieldEx does about it

  • Electrical assets on plans: switchboards, motor control centres, transformers and drives each carry their own maintenance plan and history.
  • Test values recorded: insulation resistance, thermography temperatures and other readings are entered as numbers on the job.
  • Condition visible: the asset's status and its last and next maintenance dates are shown on its record and the plan.
  • Reports for the safety programme: completed electrical maintenance can be reported by asset type, location and period.

Which maintenance KPIs should a manufacturing plant track?

PNNL's KPI guide (December 2020) gives targets alongside the availability and downtime figures. Backlog, meaning work orders in backlog status over total work orders, should be below 5% and trending down. Rework should be below 3%, and more than 95% of work orders should have a defined schedule. Schedule compliance is the number of scheduled work orders completed in a given period, normally one week, and KPIs should be reviewed at least annually.

These only mean something if every job, planned or not, passes through the same system.

What FieldEx does about it

  • Backlog on screen: unassigned jobs sit in the scheduler backlog, and open jobs are listed with their status on the dashboard.
  • Schedule compliance by week: job reports grouped by week show scheduled jobs against those completed.
  • Rework spotted: the repeat-job alert flags a new job on a machine that had a recent one, so returning faults are seen when they are raised.
  • KPIs on a schedule: saved reports with counts, sums and averages are emailed weekly or monthly to the people who review them.

How should a Malaysian plant measure planned maintenance and downtime?

There is no Malaysian benchmark, so international guidance is the usual reference. PNNL's guide on applying key performance indicators for the US Department of Energy (December 2020) sets availability above 90% and the ratio of unplanned to planned downtime below 25%. PNNL's maintenance approaches benchmarks (July 2021) give target ranges of 20-30% reactive, 25-35% preventive and 30-40% predictive maintenance as opportunities for improvement.

Those figures are a direction of travel. The first step is to log every breakdown so the plant knows its own starting point.

What FieldEx does about it

  • PM and breakdowns counted separately: each job has a type and shows whether a PM plan generated it, so reports split planned from reactive work.
  • Monthly trend reports: saved reports group jobs by type and month, and are emailed to management on a timetable.
  • Breakdown time logged: check-in and check-out times show how long each breakdown job took. FieldEx reports total downtime, MTBF and MTTR for every machine.
  • Status across the plant: the dashboard shows how many machines are running, under PM or in breakdown.
Customer story

Agri Sumber Prestari (ASP), an agricultural manpower and training company under SD Guthrie Agri Bio, with 92 estates running on FieldEx, moved its machine maintenance off logbooks and paper checklists. Its story describes work orders, inspection checklists and SOPs generated automatically, preventive maintenance triggered by usage or time, and live dashboards of job progress and stock levels with low-inventory alerts.

Read the Agri Sumber Prestari story

Magnum moved its operations off paper forms and inventory sheets onto FieldEx. Its story describes work orders, inventory logs and reports generated automatically, reports sent out on the schedule the team sets, live tracking of team activity, stock levels and job progress, and SLA alerts as deadlines approach.

Read the Magnum customer story

Questions plant maintenance managers ask about FieldEx

What is the best manufacturing maintenance software for a plant maintenance team?

One that runs planned maintenance, takes breakdown requests from the floor, keeps statutory inspections and spares, and reports downtime and cost per machine. FieldEx does all of these in one system. See our guide to choosing maintenance software.

Can maintenance be scheduled by cycle count as well as hours?

Yes. Meter units include hours, cycles and distance, and a plan can trigger on the meter, the calendar or whichever comes first.

Can operators report a breakdown without a login?

Yes. Scanning the QR label on the machine opens a breakdown form, and the request arrives as a job in the backlog.

Can FieldEx separate planned work from breakdowns in reports?

Yes. Each job has a type and shows which plan generated it, so reports can group planned and reactive work by period, line or machine.

Can we track parts for each machine?

Yes. Parts used are recorded on each job and the machine, with prices, and store stock has reorder and low-stock alerts.

Can technicians record readings such as temperatures and vibration?

Yes. Number fields on the job capture exact readings, and meter readings on the machine build a history over time.

Can we plan maintenance around shutdown weeks?

Yes. Fixed calendar schedules can be anchored to a weekday, a date or an ordinal weekday, and jobs can be created a set number of days ahead.

Can the maintenance manager see who is working on what?

Yes. The scheduler shows each technician's jobs by day or week, and managers see task status, check-ins and locations for their team.

Does FieldEx keep a history of every change to a machine's record?

Yes. Each asset has a change history showing who edited which field and when.

How quickly can a plant get FieldEx running?

Once we know your requirements and your data is ready, FieldEx can be implemented in as little as a week with standard features for small businesses. Larger setups and custom work take longer. Setup, data upload and training are included in the subscription, with no setup fee. Machines and parts can be uploaded. FieldEx helps with setup, and training is included. See FieldEx implementation.

See your plant's planned work, breakdowns and inspections in one system

Book a demo